Visual inspection - lighting for manual control

Visual inspection is a key element of industrial quality control. Despite the increasing use of automated machine vision systems, visual inspection by trained personnel remains indispensable—especially for complex inspection tasks or processes that are difficult to automate.

Our specially developed LED lights for visual inspection provide optimal lighting conditions for precise and reliable results. Designed specifically for backlight and incident-light inspection, they facilitate the detection of defects, surface irregularities, and material differences.

Thanks to modern LED technology, our lighting solutions provide uniform illumination, high contrast, and comfortable working conditions that reduce eye strain. This improves inspection quality while also increasing employee efficiency.

The LED lights are also ideally suited for industrial workplace and assembly lighting. Compared with conventional workplace lights, they provide more comfortable lighting and uniform illumination across the entire work area.

Your benefits at a glance:

  • Optimal lighting for visual inspection
  • Ideal for backlight and incident-light inspection
  • Uniform, glare-free LED illumination
  • Improved inspection accuracy and efficiency
  • Ideal for workstations and assembly areas

Transmitted light

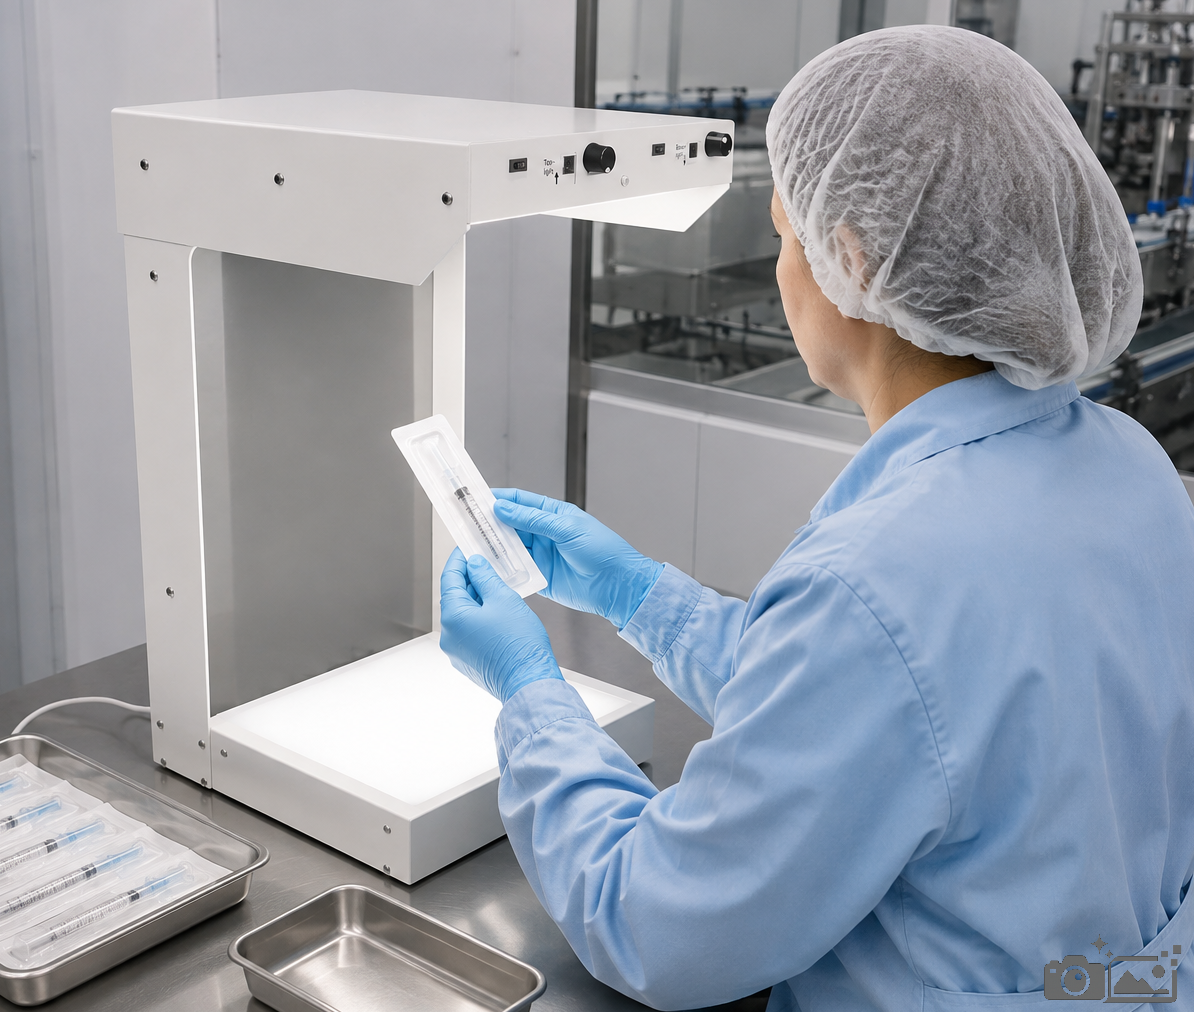
  • For transillumination and edge examination of objects
  • Rugged aluminum case in “neutral gray” color
  • No raised edge, matte finish
  • Standard light fittings D30, D40, D50 and D65
  • No IR or UV component in the light spectrum
  • With manual or digital controller

Find out more...

Light cabins

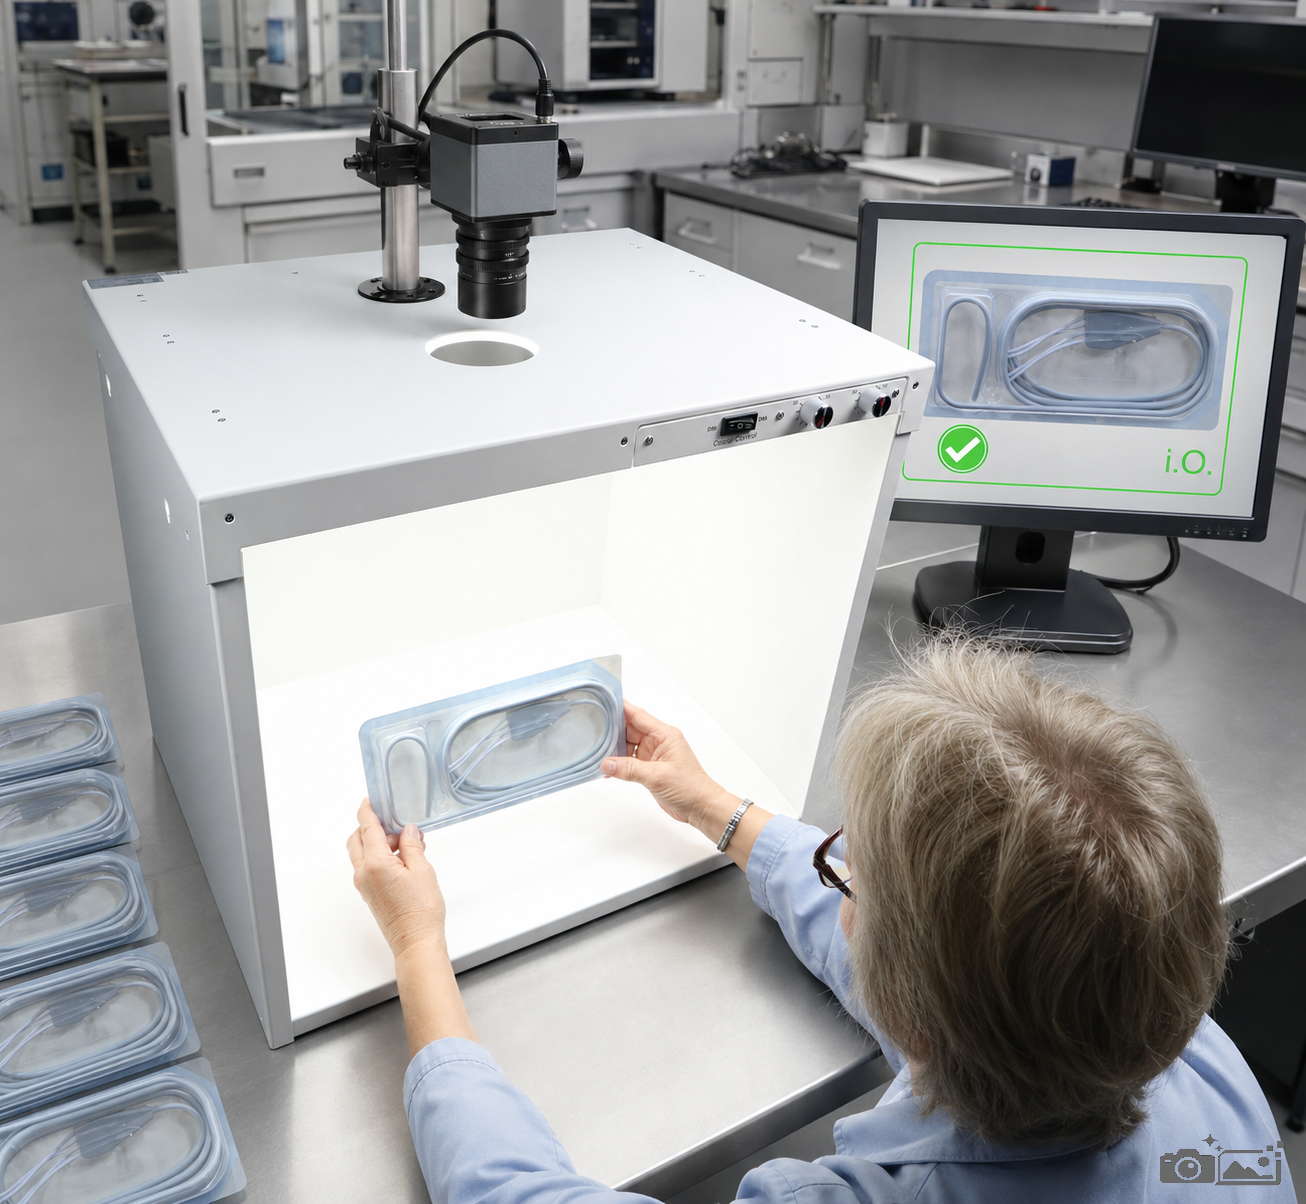
  • Light booth for testing in a controlled environment
  • Glare-free reflector system for uniform illumination
  • Standard light fittings D30, D40, D50 and D65
  • No IR or UV component in the light spectrum
  • In 1 or 2 standard light colors, switchable and dimmable

Find out more...

Reflected light

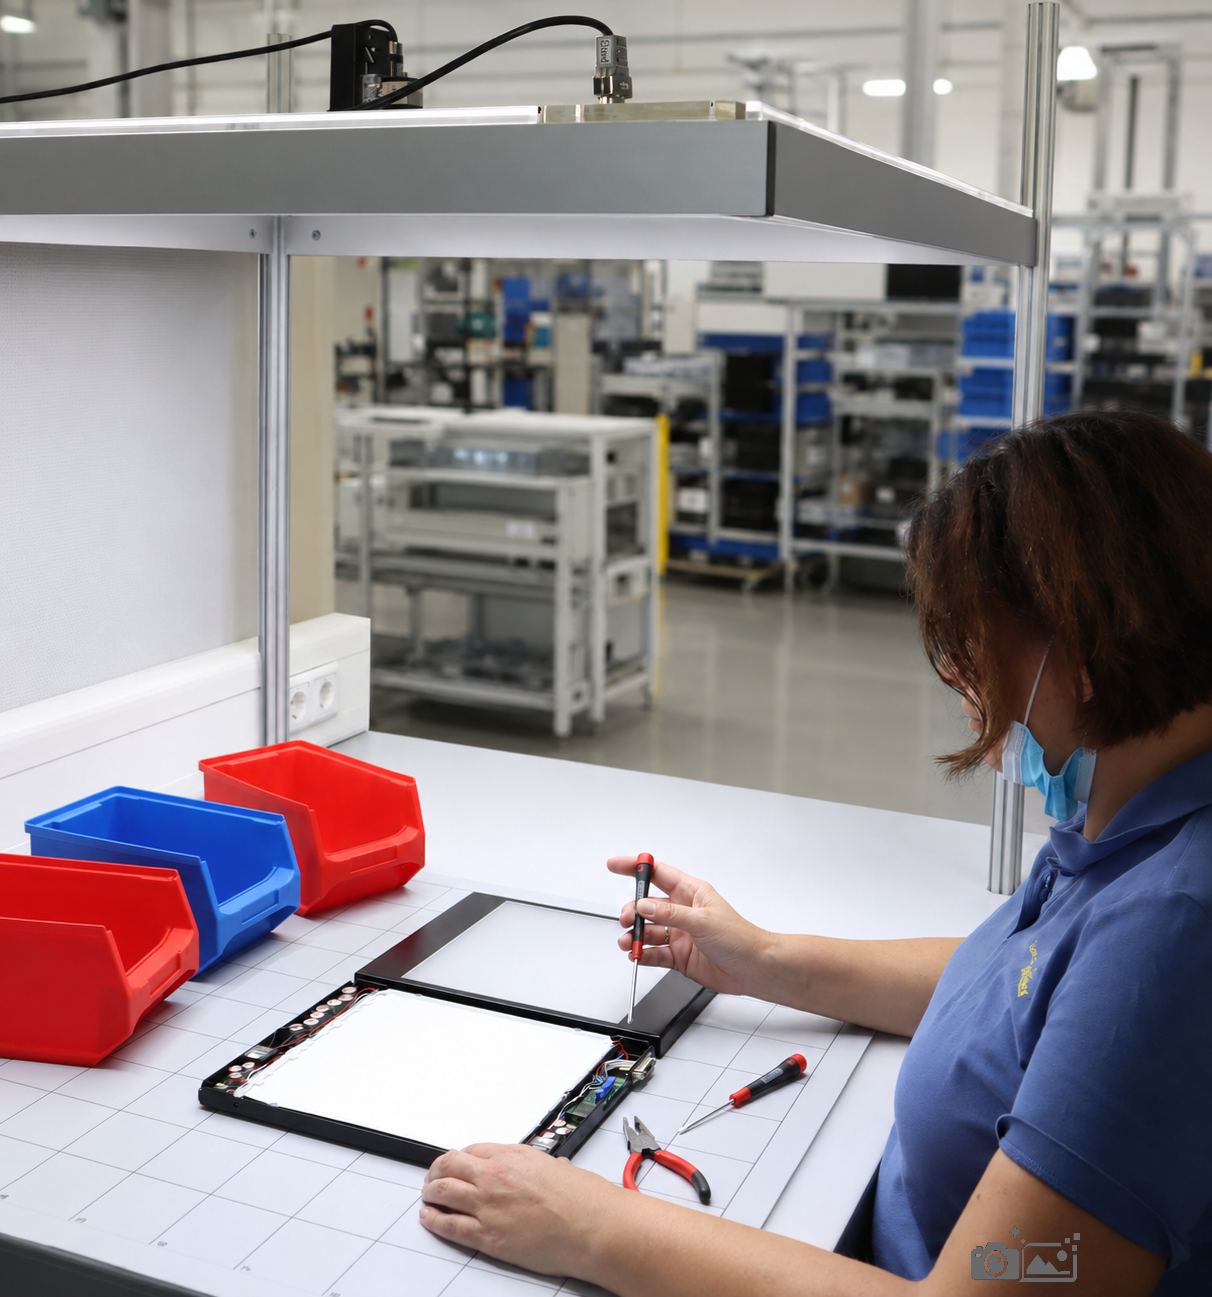
  • Normal light inspection lights for reflected lighting examination
  • Work and assembly light
  • Glare-free reflector system for uniform illumination
  • Standard light fittings D30, D40, D50 and D65
  • No IR or UV component in the light spectrum
  • In 1 or 2 standard light colors, switchable and dimmable

Find out more...

Lighting for industry 5.0

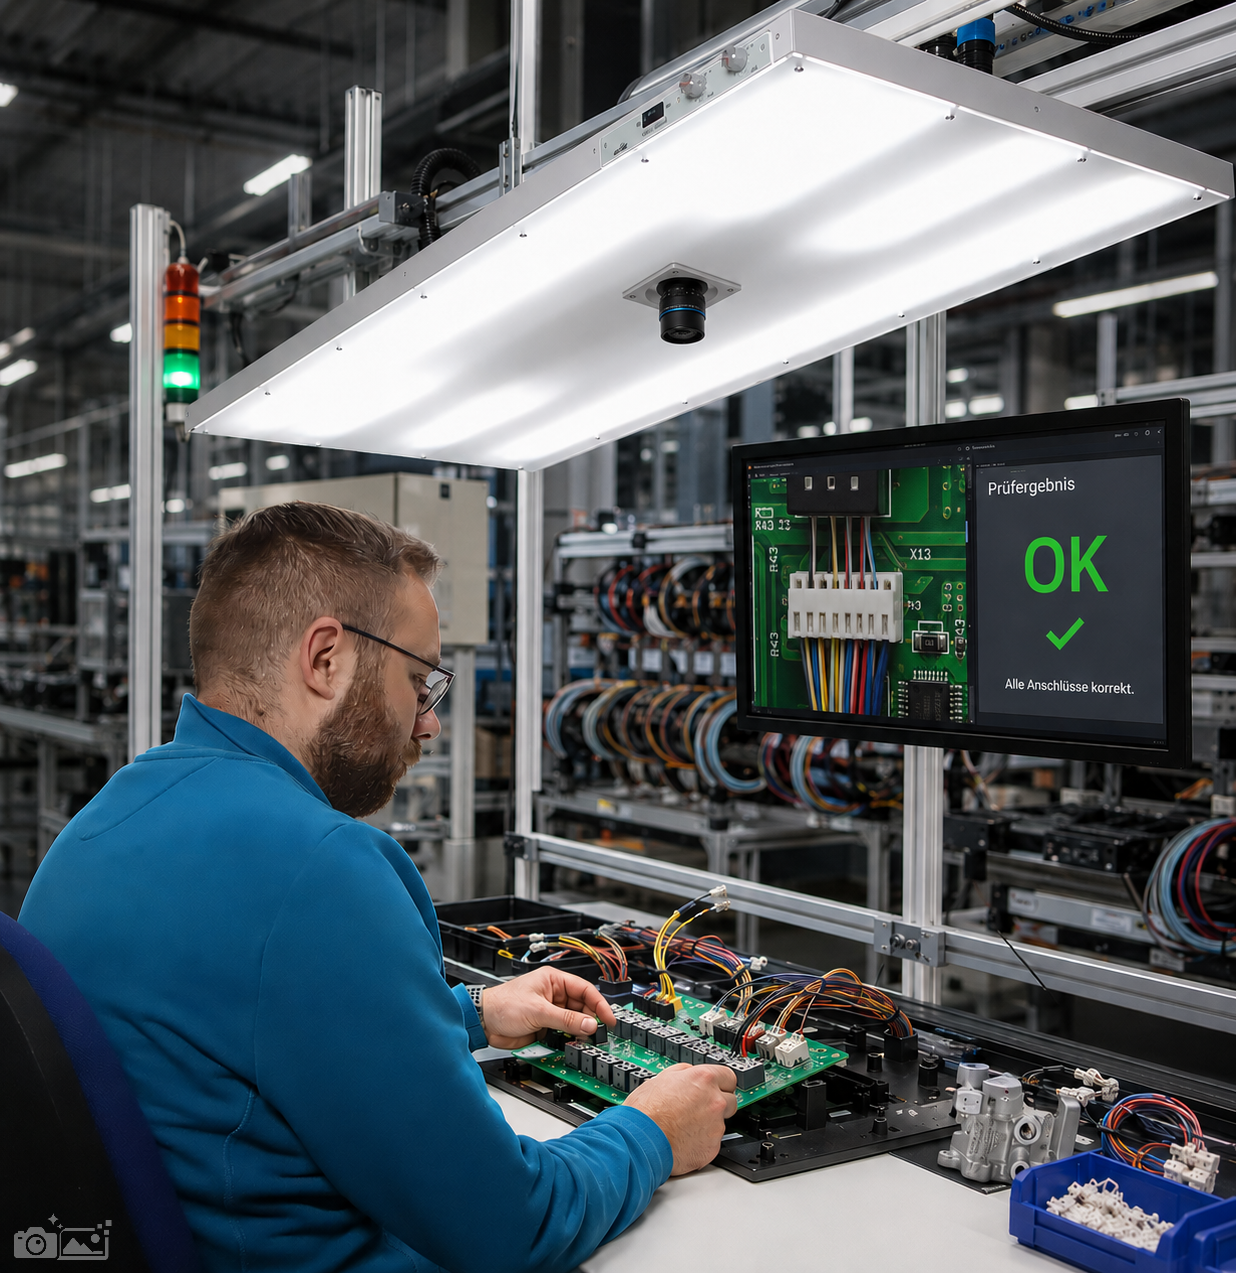
  • LED lighting for work and assembly station systems with integrated AI for real-time detection of irregularities
  • Individual adaptation to the inspection task
  • Completion of the assembly station with signal indicators for direct communication with the worker

Find out more...

In industrial quality control, a clear distinction must be made between visual inspection by employees and automated inspection using camera systems. Each method places different demands on the lighting. Manual visual inspection in particular requires a specially adapted lighting solution.

For visual inspection by employees, the following factors play a crucial role—often even more so than in industrial machine vision:

  • Light intensity – for optimum visibility of details
  • Light colour – for reliable detection of colour deviations
  • Light quality – for high-contrast, glare-free illumination
  • Arrangement of the lighting – for uniform illumination of the inspection area
  • Individual adjustability – tailored to the needs of each employee

Reliable visual quality inspection is only possible when all these factors are optimally coordinated.

As experienced lighting specialists, we have been developing customised solutions for industrial visual inspection for many years. The planistar product range is specifically designed to meet the requirements of manual quality control.

In addition to standardised solutions, we also offer customised LED lighting for visual inspection, precisely tailored to your application, inspection tasks and workstations.

Why by a human and not with the help of image processing?

Visual inspection—often referred to as VT (Visual Testing)—is an optical method of non-destructive testing and a key element of industrial quality control.

Although industrial machine vision is becoming increasingly important, it is ultimately based on analysing pixels according to predefined algorithms and criteria. Camera systems detect patterns, contrasts and deviations, but always operate within clearly programmed limits.

The human eye, on the other hand, is an extremely powerful and flexible “measuring instrument”. It can:

  • detect even the finest details and deviations
  • assess complex visual impressions as a whole
  • make decisions based not only on fixed rules, but also on experience and intuition

This human ability to assess and interpret visual information is difficult to replace entirely with software.

For this reason, sensitive industries such as the medical device industry frequently use a two-stage inspection process. An automated inspection using a machine vision system is performed first, followed by an additional visual inspection by trained personnel to ensure the highest quality standards.

Combining modern technology with human expertise provides maximum safety and reliability in quality inspection.

Visual inspection using top- or backlighting?

In visual inspection (VT – Visual Testing), choosing between incident light and transmitted light is essential for achieving optimum illumination. The most important factors are the inspection object and the features to be inspected, such as:

  • presence and completeness
  • damage
  • position and surface quality

A requirements specification should document all inspection criteria and work steps involved in the non-destructive testing process.

The inspection environment is equally important. Ambient light, inspection time and available space can all influence the result.

Drawing on our extensive experience in LED lighting for visual inspection, we develop individually tailored solutions for precise and reliable visual quality control.

Direct or indirect visual inspection

During a direct visual inspection, the inspector examines the relevant area with the naked eye. The analysis, assessment and decision are carried out directly by the person performing the inspection.

An indirect visual inspection uses a camera to display the inspection image on a monitor. This enables:

  • magnification and detailed analysis
  • visual enhancement of relevant features
  • documentation and archiving
  • simultaneous assessment by several people

Both methods offer distinct advantages: direct visual inspection allows fast and flexible decisions, while indirect visual inspection supports detailed analysis, documentation and traceability.

It's all about the right lighting

Visual inspection is strongly influenced by the human factor, including the inspector’s visual acuity, experience and accuracy. Our specially developed LED lighting solutions help compensate for factors such as fatigue, contrast conditions, colour perception and viewing angle.

Optimum illumination is essential for achieving reproducible and reliable results in manual visual inspection.

More information about standard light applications

Standard light sources for visual inspection

When visually inspecting coloured materials, selecting the correct standard light source is essential. Our colour control series is based on established standards such as DIN ISO 3664 and DIN EN ISO 3668.

Typical standard light sources:

  • D30 (3000 K) – warm light similar to incandescent lighting, often beneficial for detecting defects in different materials
  • D40 (4000 K) – less commonly used, but suitable for specific applications
  • D50 (5000 K) – the standard light source in the graphic arts industry, providing defined conditions for colour assessment
  • D65 (6500 K) – simulates daylight for comparing coloured materials

Important standard requirements:

  • Daylight-like colour temperature between 3000 and 6500 K
  • High colour rendering index (Ra > 90; planistar approximately Ra > 97)
  • Neutral, matt surroundings in light grey
  • Incident-light illumination between 2000 and 4000 lx
  • Ideally, inspection objects should be assessed under several lighting conditions

Practical tip:
D65 corresponds to overcast midday light, while D50 resembles evening light with a lower blue component. For precise colour inspection, the inspection object should be assessed under both light sources.

Not all whites are the same

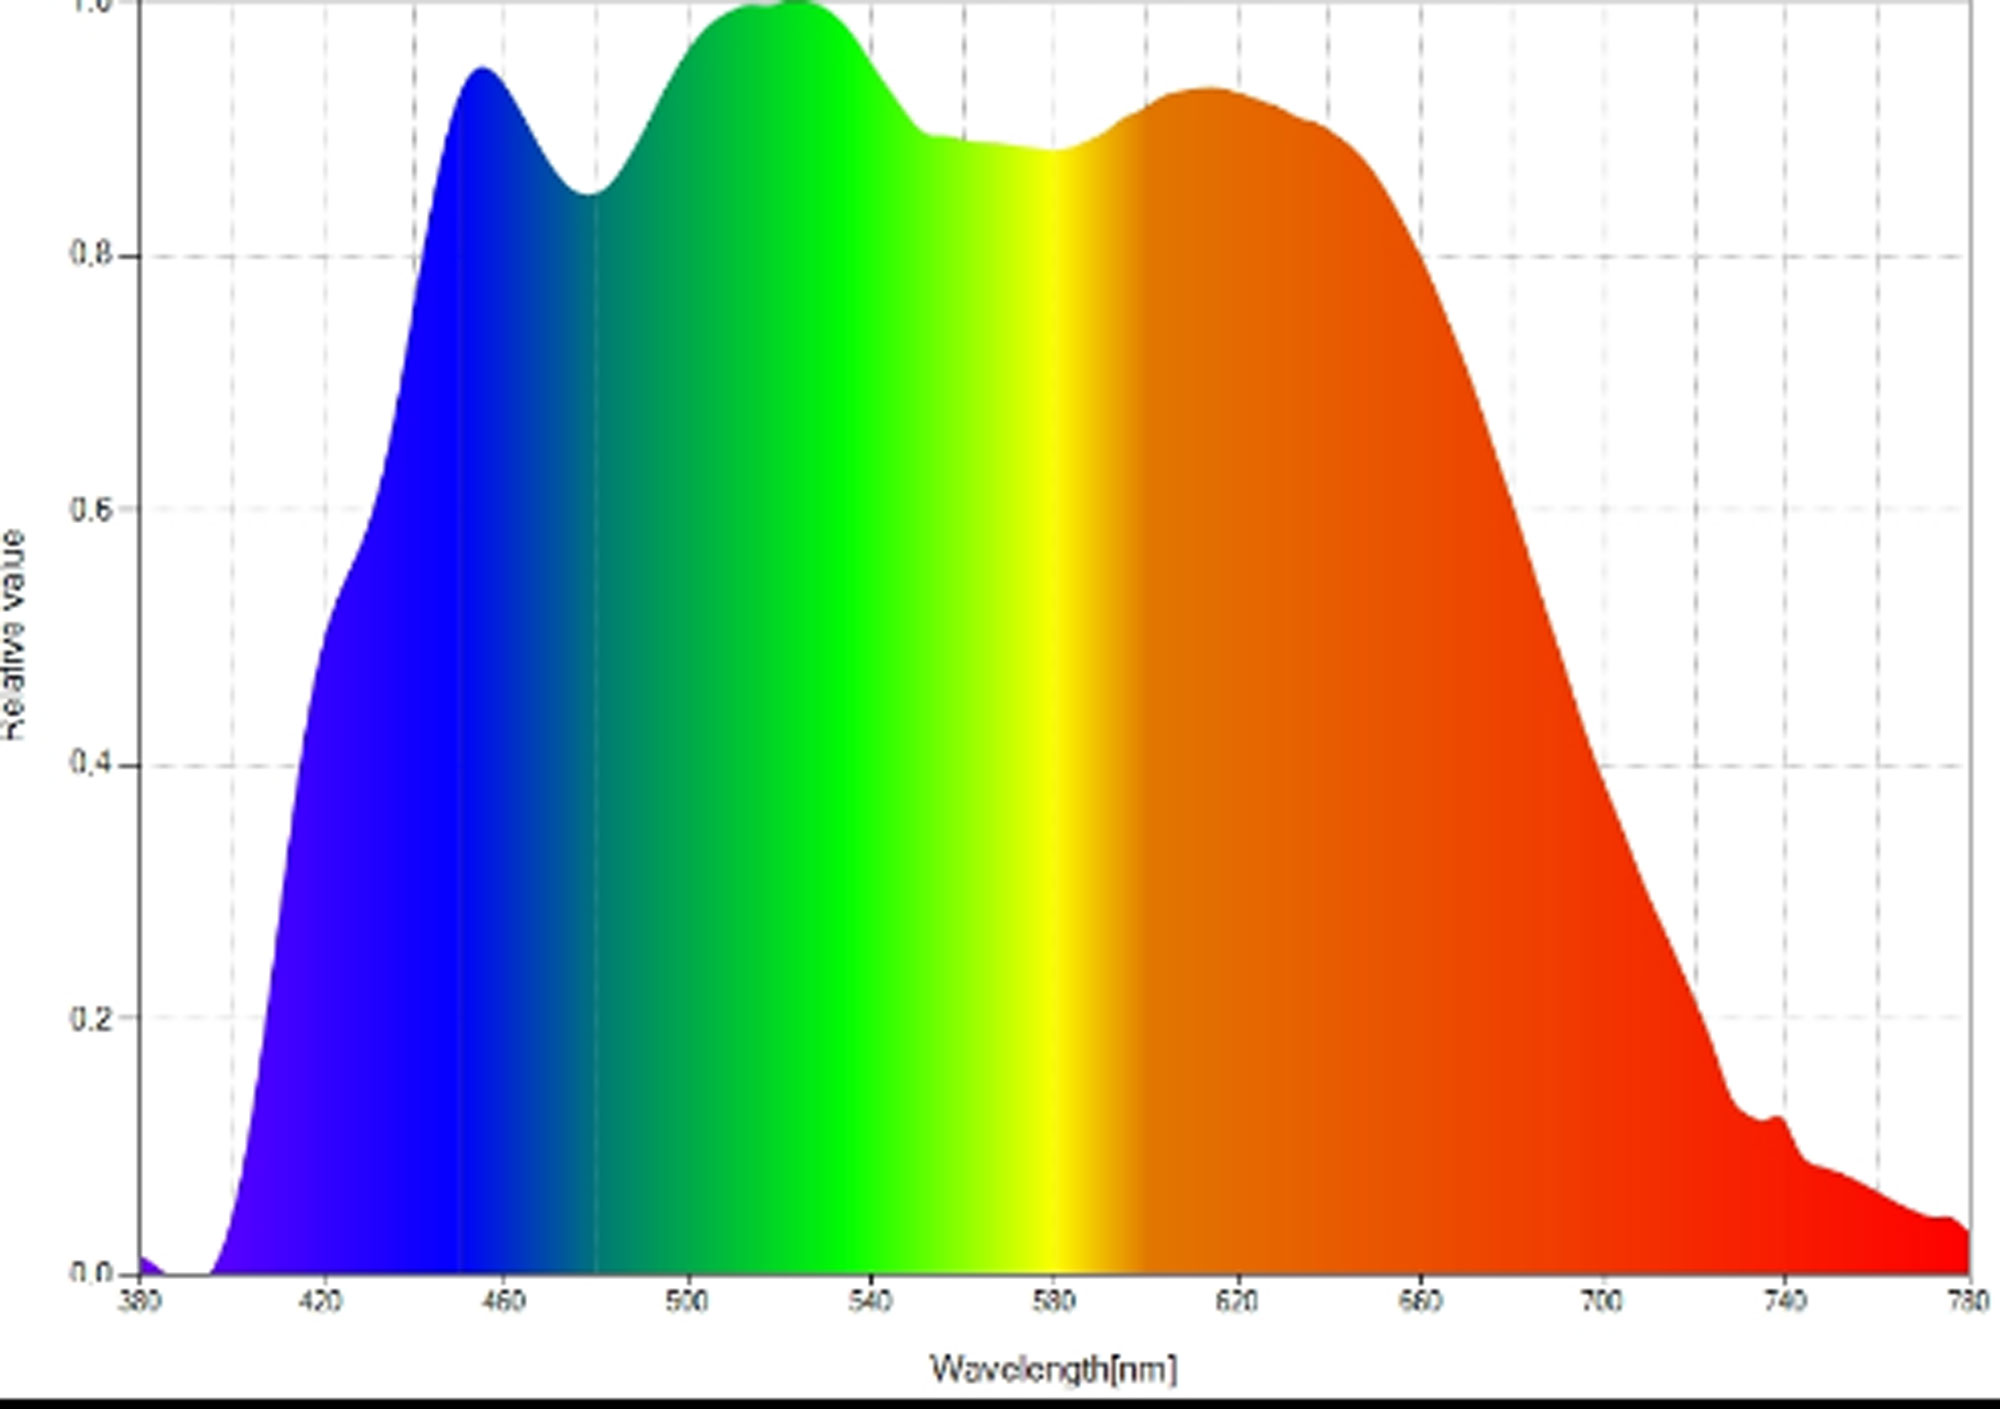
For reliable colour assessment, the light spectrum is crucial. Only colours contained within the light emitted by the source can be correctly reflected by the inspection object and perceived by the observer. An inadequate spectrum therefore results in distorted colour reproduction.

Ideally, the spectrum of a light source should approximate natural sunlight (CRI = 100) as closely as possible. However, the colour characteristics of daylight change depending on the time of day and season.

  • Evening daylight (5000 K) compared with
  • Midday daylight (6500 K)

    → Colours can appear significantly different under these lighting conditions (see example).

Choosing the correct standard light colour is therefore essential for precise visual colour inspection.

Any questions?

Our team will be at your disposal for any questions you may have. We will process your request as soon as possible.

+49 (0) 9364 8060-0sales@no-spam.planistar.de Industrial Lighting Catalog (incl. prices) Visual Inspection Catalog (incl. prices)
Office hours: 
Monday - Thursday8.00 am - 04.00 pm
Friday8.00 am - 01.00 pm
  Accessories Catalog (incl. prices)
You can also find us at:Logo XING Logo Linkedin